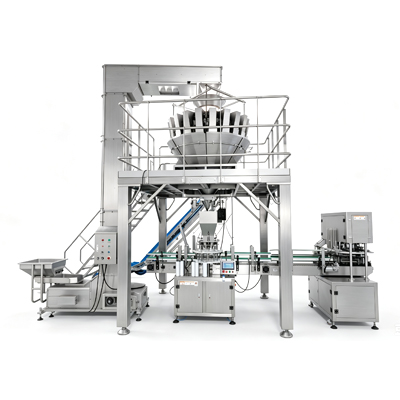
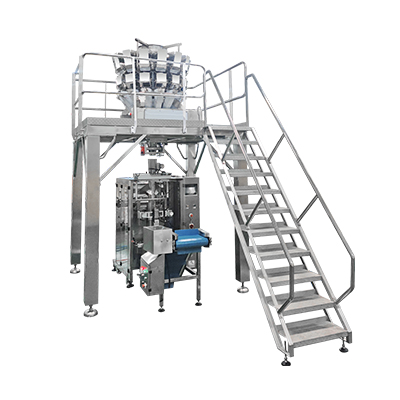
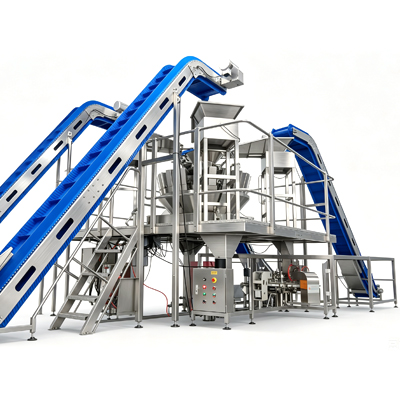
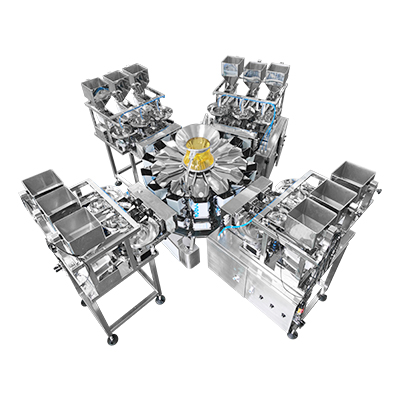
Multi-outlet Z-type Bucket Elevator | Multi-point Discharge Conveyor
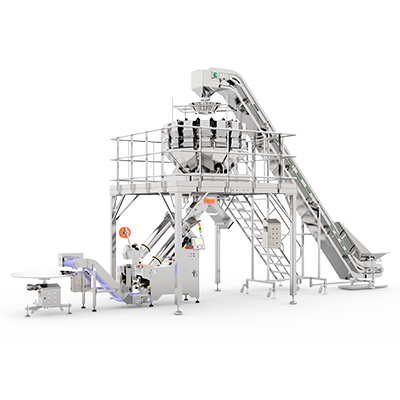
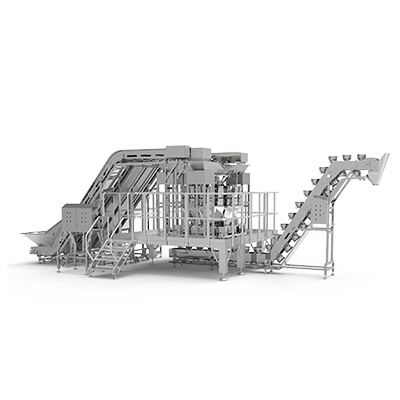
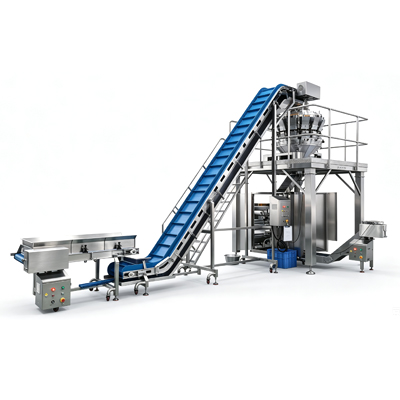
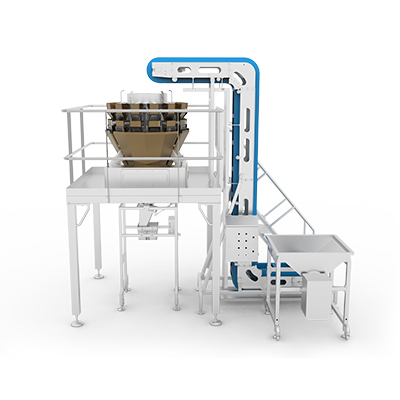
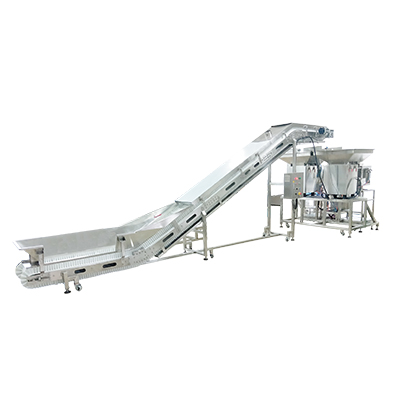
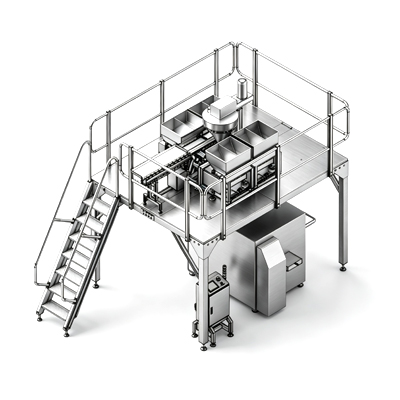
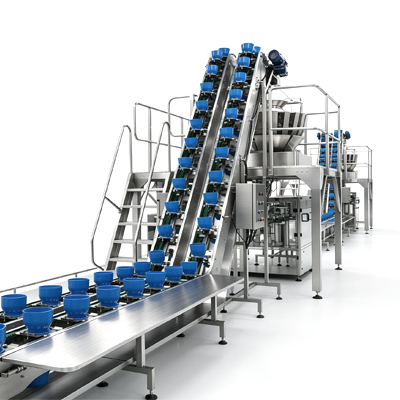
The Multi-outlet Z-type Bucket Elevator is a professional automatic conveying machine designed for multi-station quantitative feeding and zero-residue material replacement. Equipped with 5 independent discharge outlets and a built-in screw recycling channel, this Z-type bucket conveyor supports closed-loop circulating material transportation with a stable conveying capacity of 54kg/min and a standard 4L bucket volume.
Different from traditional single and multi-port lifting equipment, it automatically recycles residual materials to avoid accumulation and cross contamination. Adopting tilting bucket flexible discharging design, it ensures low material breakage and stable operation. Widely applicable to granular, lumpy and high-fluidity bulk materials, it is an ideal automatic feeding solution for food, chemical, hardware and feed industries to reduce material waste and labor costs.
Applicable Materials & Application Industries
Applicable Materials
This multi-point discharge bucket elevator fits most high-fluidity bulk materials without blocking or spilling.
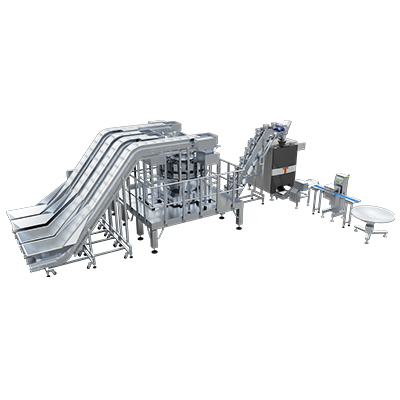
Comes with 5 independently controlled discharge ports to support synchronous multi-height and multi-station feeding. A single unit replaces multiple single-outlet elevators, greatly reducing equipment procurement and layout costs.
Closed-loop Screw Recycling & Zero Material Loss
Built-in automatic screw recycling system collects and retransports residual materials for cyclic utilization. Fully enclosed conveying avoids spilling, residue accumulation and cross contamination, saving raw materials and manual cleaning costs.
Equipped with standard 4L buckets to achieve a stable 54kg/min conveying capacity, meeting continuous production demands. Optional 304 stainless steel, food-grade plastic and carbon steel materials fit food, chemical, hardware and other industrial standards.
Integrated Z-type structure saves workshop space and adapts to various factory layouts. Flexible tilting bucket discharging lowers material breakage and running noise. Modular chain transmission design ensures stable operation and quick maintenance.
Automatic Working Process
Material Feeding
Raw materials are put into the bottom feeding port and evenly fall into the upward running buckets.
Z-type Lifting Conveying
Buckets carry materials along the Z-type track to complete vertical lifting and horizontal transmission.
Graded Multi-point Discharging
Buckets flip automatically at each discharge outlet to feed materials to corresponding production stations in sequence.
Residue Material Collection
Remaining materials after multi-point discharging fall into the tail screw recycling device.
Closed-loop Circulation Refeeding
The screw system transports residual materials back to the bottom feeding port to realize uninterrupted circulating conveying.
Q1: What materials can this Z-type bucket elevator convey?
A: It is suitable for all high-fluidity granular and small block materials such as nuts, grains, pet food, chemical particles and small hardware parts. Viscous materials need pre-test confirmation.
Q2: What is the advantage of the 5-outlet design?
A: 5 independent discharge ports support simultaneous feeding for 5 production lines, replacing multiple single-outlet machines and saving equipment investment and workshop space.
Q3: How does the residual material recycling system work?
A: Unloaded residual materials are automatically collected by the tail screw device and transported back to the feeding port for cyclic reuse, realizing zero residue and zero waste.
Q4: Will the conveying process damage fragile materials?
A: Adopting natural tilting flexible discharging without rigid collision or scraping, the breakage rate is extremely low, which is very suitable for fragile food materials.
Q5: Is the equipment easy to maintain?
A: Modular integrated design allows quick disassembly and replacement of core components. Chain transmission structure is stable with low failure rate and low daily maintenance cost.
Contact Us
Looking for a high-efficiency, zero-residue and space-saving multi-outlet Z-type bucket elevator for your production line? We provide customized design, OEM & ODM service, factory direct sales and after-sales global support.
Welcome to send inquiry for detailed parameters, quotation and free solution!
Product Description
Submit Your Requirements
Please submit your requirement form, and we will customize the most suitable solution according to your needs.
Automated mesh bagging extends produce shelf life by providing vital airflow. Upgrading your line slashes labor costs, stops product giveaway, and maximizes daily output.
Dust-controlled powder fillers use vacuum extraction and servo-driven augers to package fine materials. These automated systems prevent waste, ensure safety, and maximize ROI.
Horizontal packaging machines use lateral movement to safely package solids, powders, and liquids. These systems ensure leak-proof seals, cut labor costs, and maximize your ROI.
It is a high-tech enterprise specializing in the R&D, design, and independent manufacturing of packaging, conveying, weight detection, weighing, and filling equipment.