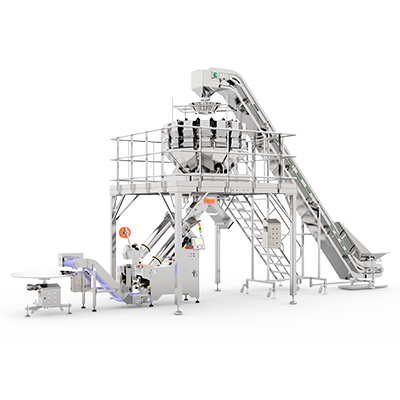
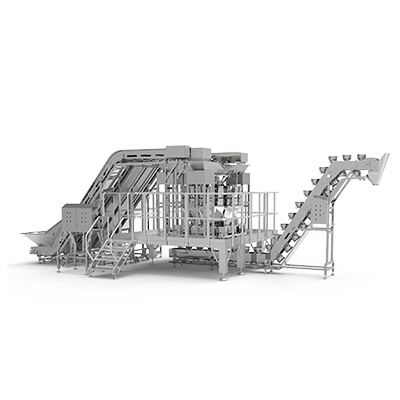
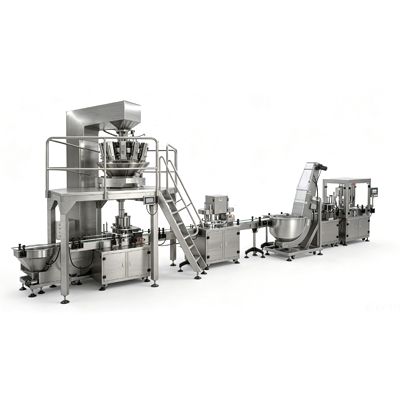
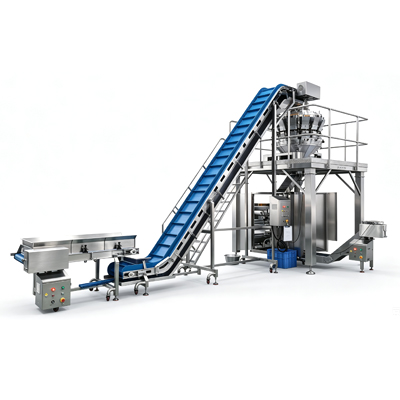
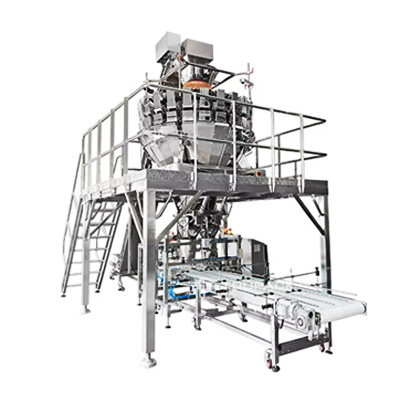
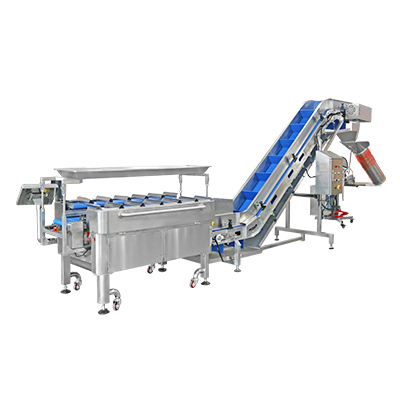
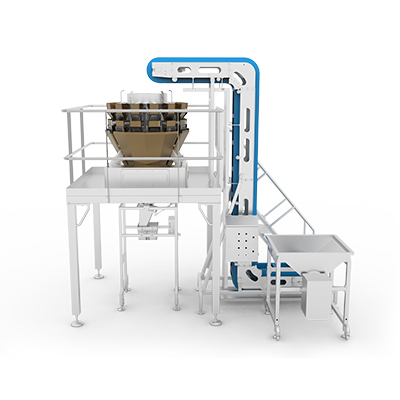
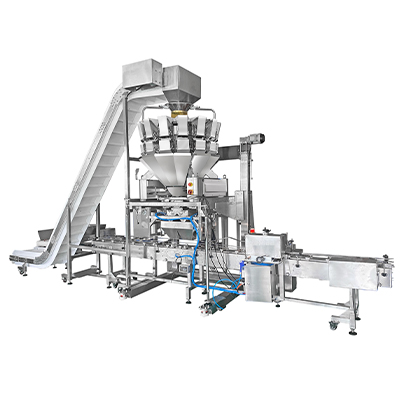
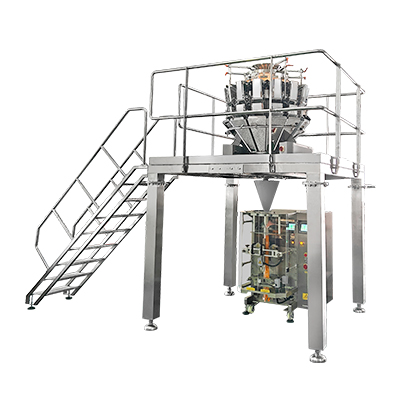
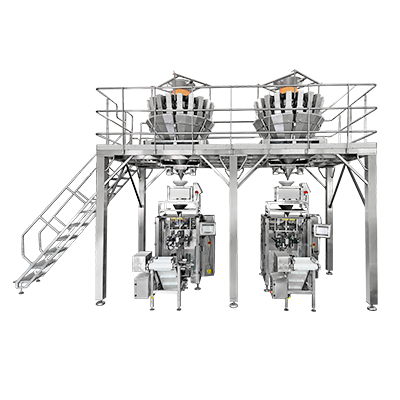
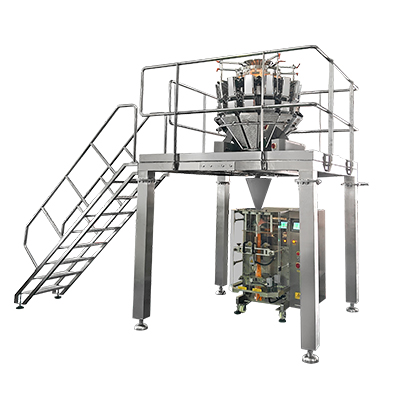
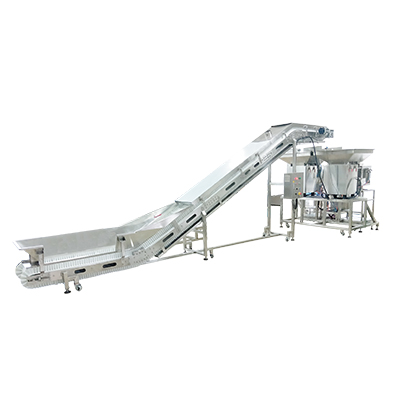
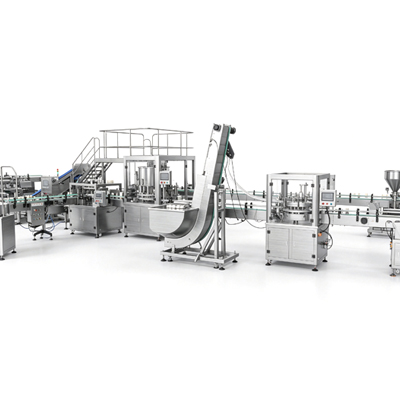
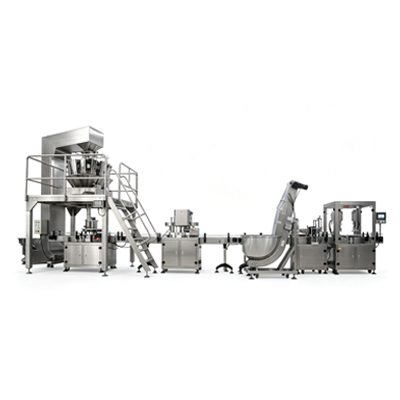
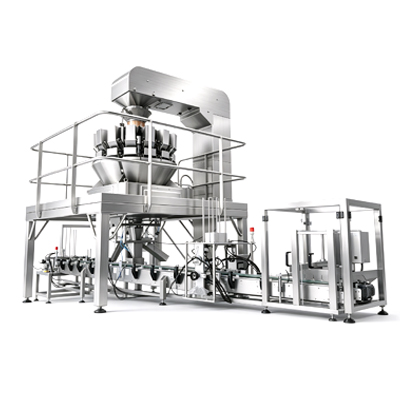
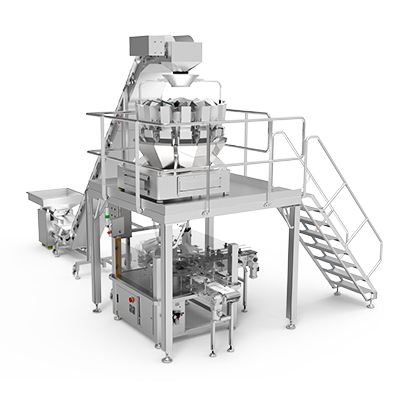
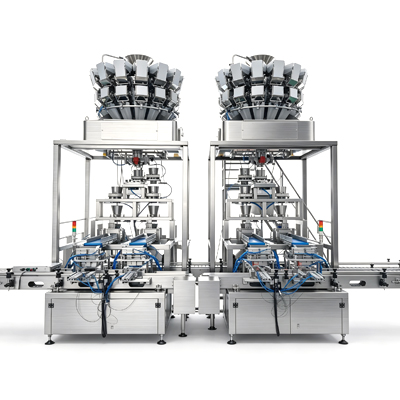
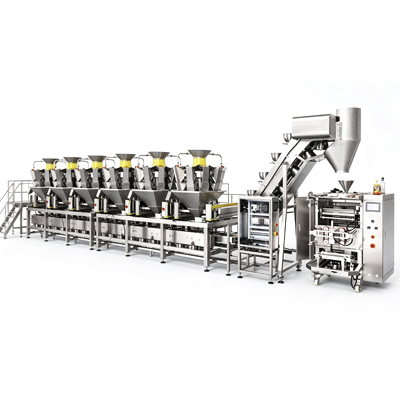
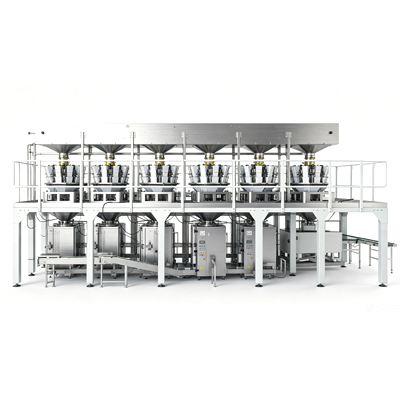
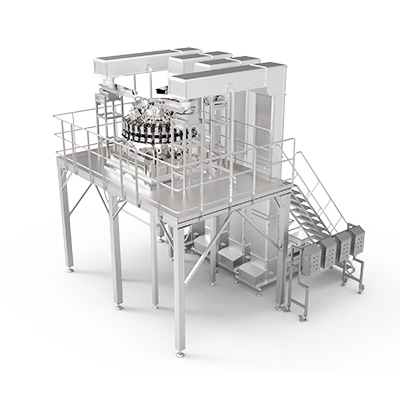
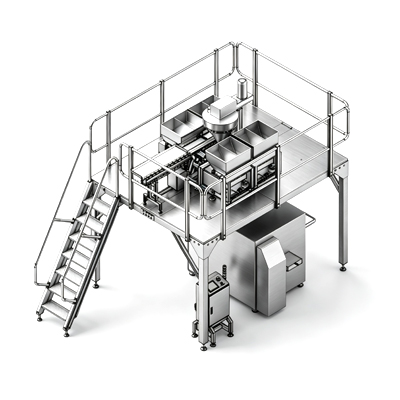
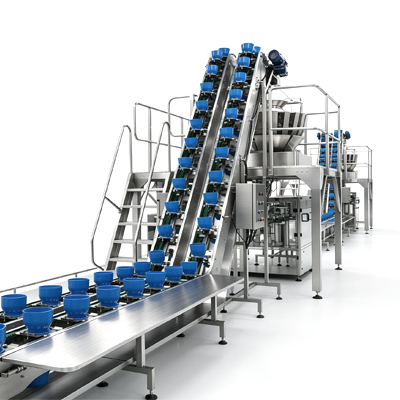
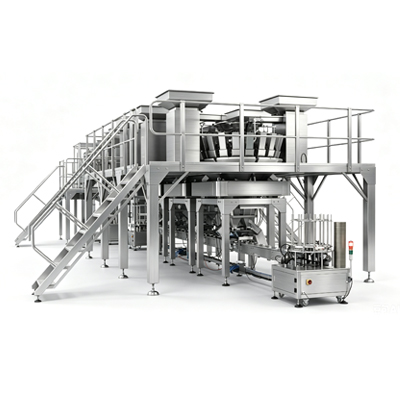
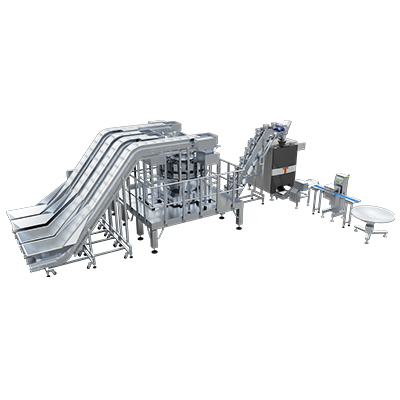
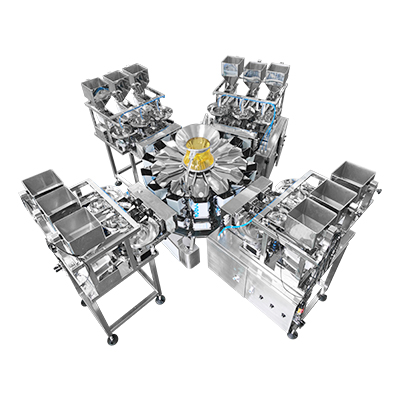
12-Head Small Fruit Weighing Cartoning Line – Twelve Parallel Lane Full-Automatic Integrated Weighing & Cartoning Production Line For 50–500g Small Berry Fruits
This integrated 12-head fruit weighing cartoning line adopts 12 parallel independent weighing lanes specially customized for fragile small berry fruits, completely different from dry granule linear weighers (3/4/6/8-head screw/vibration models). It targets standardized automated fruit processing factories that require full-line unmanned operation for small berry retail carton packaging, solving core pain points of berry agricultural processing plants, fresh fruit sorting factories and supermarket fruit packing suppliers: low throughput of 4/6/8-head single weighing machines requiring separate cartoning equipment, easy fruit extrusion & bruising caused by traditional vertical hoppers, lack of integrated feeding-weighing-cartoning-labeling function, unstable weight consistency of manual fruit packing, difficult water washing and poor dustproof performance of ordinary weighers, limited data storage for multi-spec fruit orders.
Continuous stable production speed reaches industry-leading 75 cartons per minute with X(0.5) stable weighing precision and 0.1g minimum scale interval, covering retail plastic clamshell boxes, paper fruit cartons, small berry punnet packs within the 50–500g weight range. This full-process integrated fruit weighing cartoning line serves large-scale blueberry planting processing bases, cherry tomato sorting packaging workshops, raspberry fresh-keeping packing factories and fruit wholesale automated filling production facilities.
Complete Product Overview
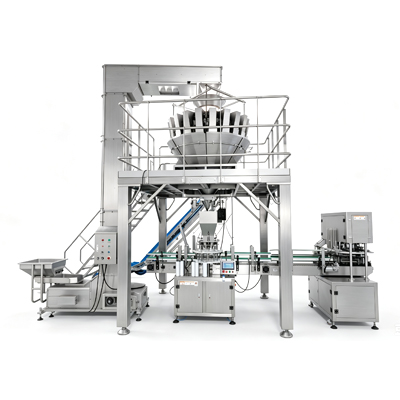
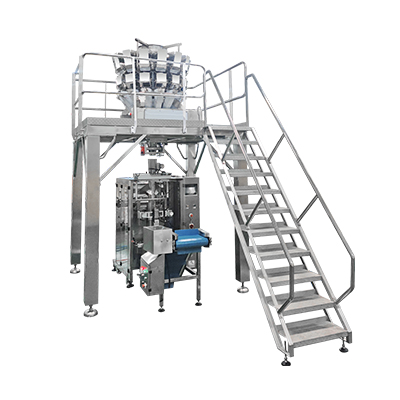
The horizontal 12-head integrated small fruit weighing cartoning line is equipped with twelve independent square anti-collision fruit hoppers (100*100mm size), built as one-piece full-automatic production line integrating automatic feeding, multi-lane weighing, carton positioning, filling, dynamic capping, coding and labeling. It adopts industrial MCU main control unit matched with 10-inch color touch HMI, pre-stored dedicated operation formulas for blueberry, cherry tomato, raspberry and other soft small berry fruits, supporting one-click parameter switching for different fruit sizes and carton specifications.
Its core differentiated competitive advantage against all dry material linear weighers and split fruit packing equipment is twelve parallel soft buffer fruit weighing lanes + all-in-one cartoning post-processing system: each lane uses wide buffer conveying trough to avoid bruising fragile berries, twelve-channel synchronous weighing greatly improves hourly carton output, whole machine reaches IP65 waterproof grade for direct flushing after fruit processing. Horizontal single-layer open frame with rotatable disassembly components realizes full dead-corner-free cleaning, all fruit contact parts are food-grade thickened 304 stainless steel and soft food-grade silicone buffer strips. The whole line adopts reinforced integrated heavy-duty frame with multi-point anti-vibration support feet to offset twelve-lane combined conveying vibration, net weight 1085kg with streamlined overall layout that balances ultra-high cartoning speed and workshop space occupation, becoming the only integrated twelve-lane high-efficiency automated weighing cartoning equipment for soft small berry fruit processing production lines.
Core Differentiated Product Advantages For 12-Head Integrated Small Berry Fruit Weighing Cartoning Line
Exclusive Twelve Independent Parallel Soft-Buffer Fruit Weighing Lanes
Twelve fully separated anti-bruising fruit feeding & high-stability weighing assemblies
Twelve groups of wide silicone buffer conveying troughs, fruit-friendly weighing sensors and 100*100mm square anti-collision mini hoppers operate independently; single lane fruit blockage will not stop the whole production line, drastically cutting downtime loss during round-the-clock continuous berry cartoning shifts.
Dual flexible automated production operation modes
Mode 1: Unified weight & conveying speed set for all twelve lanes, ultra-high-speed mass uniform fruit carton production, 2–3x higher throughput than 6/8-head split weighing equipment;
Mode 2: Separate target weight and conveying speed configured per channel, supporting mixed multi-spec berry carton filling and flexible switching of different fruit varieties without line shutdown.
Twelve-channel anti-vibration fruit weighing algorithm
Custom multi-lane weight calculation logic eliminates mutual conveying vibration between twelve fruit hoppers, sustaining steady X(0.5) weight precision without soft berry extrusion damage during all-day continuous feeding.
Integrated full post-cartoning function
Built-in automatic carton threading, dynamic capping, online coding and labeling station, no need to purchase separate cartoning machines, realizing one-stop unmanned production from raw fruit to finished labeled fruit cartons.
Twelve Sets of 100*100mm Square Anti-Collision Soft Buffer Fruit Hoppers
Each square hopper is equipped with surrounding soft silicone anti-bruising lining, matched with wide slow-speed conveying trough, effectively preventing scratch, extrusion and bruising of fragile blueberry, raspberry and cherry tomato. Fixed 100*100mm cavity size perfectly adapts conventional 50–500g retail fruit carton inner size, reducing fruit residual waste and cross-variety contamination risk during frequent switching between different berry formulas.
Industrial MCU Intelligent Control With 10 Inch Large Color Touch HMI
Pre-stored multi-group dedicated soft berry fruit formulas for blueberry, cherry tomato, raspberry, small berry varieties, one-click instant recall without repeated calibration during frequent carton spec changes;
Real-time split twelve-lane production data display: each channel’s target fruit weight, cumulative finished carton count and residual fruit volume can be individually monitored on large touch screen;
Massive data storage supports up to 99 sets of production parameter records, convenient for factory production traceability and batch quality management.
IP65 Full Waterproof Flushable Structure & Rotatable Quick-Disassembly Components
The whole line reaches IP65 high waterproof rating, allowing direct water flushing after daily fruit processing to remove fruit pulp, juice and residue. All main contact components adopt rotatable quick-release design without specialized tools for disassembly, rapidly clearing rotten fruit residue to eliminate cross-contamination risk of different fresh berry raw materials. Oversized open transparent protective baffle facilitates real-time observation of internal fruit conveying and weighing status.
Reinforced Integrated Anti-Vibration Heavy Frame Adaptable For Large-Scale Fruit Processing Factories
Integrated horizontal single-layer thickened reinforced heavy cabinet with multi-height adjustable stainless steel support stand, large anti-slip load-bearing foot pads to fit large fruit processing workshop ground. Optimized overall frame structure counteracts twelve-lane combined conveying vibration to prevent weighing drift during non-stop long-hour high-speed cartoning operation. Adapt to 0℃~40℃ temperature and 40%~90% high humidity fresh fruit workshop environment, internal electrical components with full waterproof, dustproof and moisture-proof sealing protection, stable continuous operation in blueberry, raspberry and cherry tomato automated cartoning mass production workshops.
Optimized Low Unit Power Consumption For Round-The-Clock 75bpm High-Speed Cartoning Production
Total rated power only 2.8kW, far lower comprehensive energy consumption than deploying multiple sets of split 6-head weighing + independent cartoning machines to match equivalent twelve-lane throughput, significantly cutting monthly electricity operating costs for large-scale berry fruit processing manufacturers.
Applicable Industries & Corresponding Fragile Small Berry Fruit Materials
This twelve-lane integrated full-automatic 12-head small fruit weighing cartoning line with twelve anti-collision soft buffer 100*100mm fruit hoppers is exclusively engineered for uninterrupted high-speed synchronous automated cartoning of fragile soft small berry fruits, covering mini retail punnets to medium fruit cartons within the 50g–500g weight band. It delivers stable twelve-lane one-stop weighing, filling, capping and labeling integrated production for large blueberry planting processing bases, cherry tomato sorting factories, raspberry fresh-keeping packaging workshops and comprehensive fresh fruit wholesale automated filling lines.
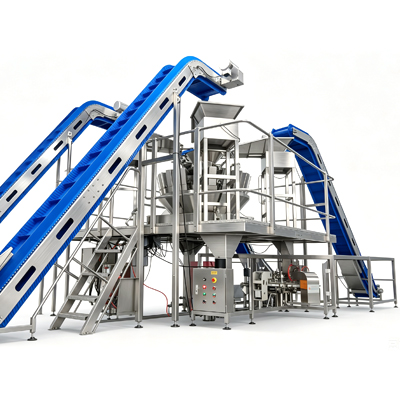
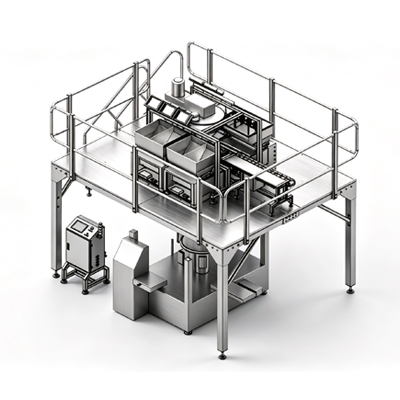
Horizontal single-layer twelve independent parallel soft-buffer fruit conveying & weighing channels + integrated automatic cartoning capping labeling post-processing station
Note: All listed parameters are factory standard configuration. Fruit conveying speed, carton positioning size, hopper silicone soft strip thickness and touch screen multi-language version can be customized according to berry fruit softness, carton punnet size and full-line unmanned production layout demands. Supporting carton threading, online inkjet coding and dynamic labeling modules can be upgraded and expanded on-site.
Working Principle of 12-Head Integrated Twelve-Lane Small Fruit Weighing Cartoning Line
This horizontal integrated 12-head small fruit weighing cartoning line adopts twelve fully isolated soft buffer fruit conveying and high-stability weighing assemblies matched with 100*100mm anti-collision fruit hoppers, specially optimized for synchronous high-speed weighing and automatic cartoning of fragile soft small berry fruits.
Raw picked berry fruits are evenly fed into the shared top wide buffer feeding conveyor and distributed to twelve independent square fruit storage hoppers; each lane’s slow-speed soft silicone buffer trough transports fragile berries gently into its own fruit weighing cavity without cross-lane fruit mixing or mutual conveying vibration signal interference. The built-in industrial MCU control system independently collects real-time fruit weight data from each channel’s high-stability load cell and executes twelve-lane synchronous intelligent conveying speed adjustment logic:
Automatically reduce conveying speed when fruit weight nears preset carton target value to guarantee unified X(0.5) stable precision across all twelve channels without berry bruising;
When all twelve channels reach standard carton target weight, synchronous bottom fruit discharge gates open, soft berries slide down into pre-positioned empty fruit cartons; cartons are automatically conveyed to post stations for dynamic capping, inkjet coding and labeling to form finished packaged fruit products.
The horizontal twelve independent soft buffer hopper + all-in-one cartoning station integrated design achieves 75bpm ultra-high continuous cartoning speed, far exceeding split single-function fruit weighing machines; partial continuous cartoning production can be maintained if single lane jams, avoiding full line shutdown loss, greatly boosting equipment round-the-clock continuous operation efficiency for large-scale soft small berry automated fruit processing workshops.
Measurable Production Efficiency & Cost Upgrade Benefits For Large-Scale Small Berry Fruit Processing Manufacturers
Twelve-lane synchronous integrated line maximizes hourly finished fruit carton throughput
Single all-in-one twelve-head line realizes 2–3 times the output of split 6/8-head weighing + separate cartoning equipment, reducing factory total equipment procurement quantity and occupied workshop floor space.
Direct water flushing eliminates manual scrubbing of fruit juice and pulp residue, rotatable quick-disassembly components cut daily maintenance time and spare parts stocking expenses.
Soft silicone buffer anti-bruise structure lowers fruit waste loss rate
Gentle slow-speed conveying avoids extrusion damage of high-value blueberry, raspberry and cherry tomato, drastically reducing raw fruit scrap loss compared with ordinary vibration fruit weighers.
One-stop integrated feeding-weighing-cartoning-labeling saves extra auxiliary equipment investment
No need to purchase independent cartoner, capper and labeling machine separately, one single production line completes all finished product processing steps, lowering overall factory automation investment cost.
Uniform retail carton net weight eliminates supermarket customer complaints and market supervision unqualified risks for mass exported and domestic retail soft berry fruit bulk orders.
12-Head Small Fruit Weighing Cartoning Line (100*100mm Anti-Collision Fruit Hopper) – Twelve-Lane Integrated High-Speed Soft Berry Automated Weighing & Cartoning Solution For Blueberry, Cherry Tomato, Raspberry 50–500g Retail Fruit Punnet Carton Full Production Line
This industrial integrated fruit automatic weighing cartoning production line is not any dry granule 3/4/6/8-head linear weigher, single-lane fruit filling machine, split separate fruit cartoner, medium/jumbo bag grain bulk weighing equipment or heavy industrial powder filling scale, but a horizontal single-layer twelve-parallel-channel soft fragile small berry exclusive all-in-one weighing cartoning automated production asset built for large agricultural fruit processing factories pursuing maximum hourly carton throughput and full unmanned one-stop finished fruit production. Equipped with twelve 100*100mm soft anti-bruise buffer fruit hoppers, independent gentle fruit conveying weighing system and industrial MCU large touch screen intelligent control, it is the optimal IP65 waterproof low-energy high-efficiency integrated cartoning equipment for large fruit factory uninterrupted soft small berry retail punnet high-speed automated packaging lines.
We provide free twelve-lane synchronous soft berry X(0.5) high-precision weighing cartoning on-site trial test for all blueberry planting processing, cherry tomato sorting and raspberry fresh-keeping packaging factory clients. Contact our sales team to obtain an exclusive horizontal twelve-lane integrated high-speed small fruit weighing cartoning full production line solution and factory-direct quotation!
Disclaimer: Machine renderings, engineering dimension drawings and all technical parameters displayed on this page are for reference purposes only. Please consult our professional sales engineer to confirm customized specifications matching your berry fruit softness, retail fruit carton punnet size, multi-variety mixed fruit packing layout and hourly 75bpm finished carton throughput demands.
Product Description
Submit Your Requirements
Please submit your requirement form, and we will customize the most suitable solution according to your needs.
Automated mesh bagging extends produce shelf life by providing vital airflow. Upgrading your line slashes labor costs, stops product giveaway, and maximizes daily output.
Dust-controlled powder fillers use vacuum extraction and servo-driven augers to package fine materials. These automated systems prevent waste, ensure safety, and maximize ROI.
Horizontal packaging machines use lateral movement to safely package solids, powders, and liquids. These systems ensure leak-proof seals, cut labor costs, and maximize your ROI.
It is a high-tech enterprise specializing in the R&D, design, and independent manufacturing of packaging, conveying, weight detection, weighing, and filling equipment.