You are here:Home / Case Studies / Daily Food / Automatic Rice Weighing Packaging & Checkweighing Production Line
loading
Automatic Rice Weighing Packaging & Checkweighing Production Line
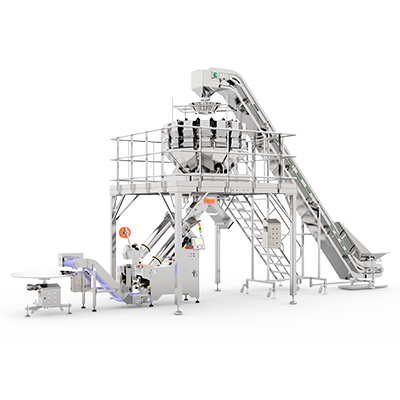
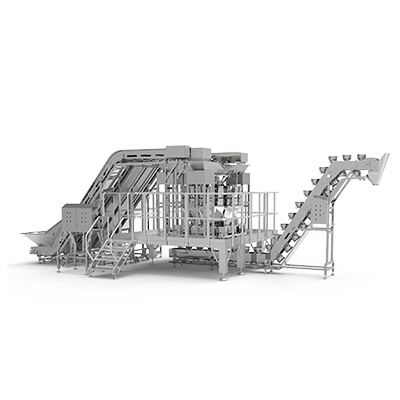
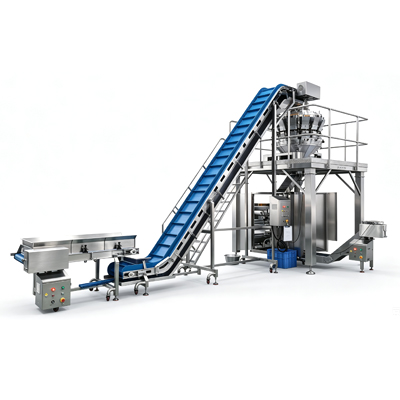
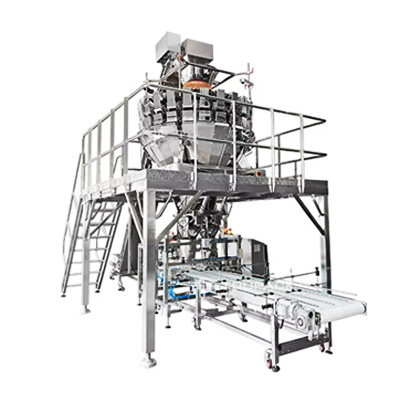
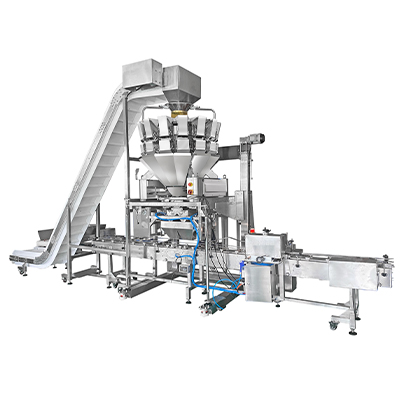
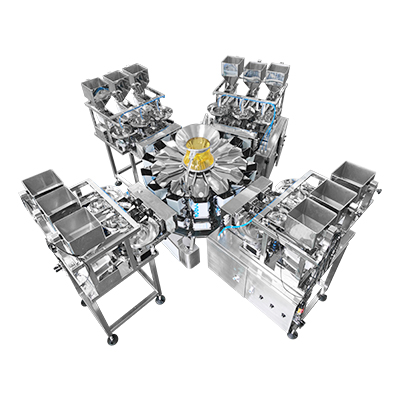
Fully automatic rice weighing and packaging production line equipped with 20-head multihead weigher, VFFS machine, Z-type elevator and automatic checkweigher, 100% weight inspection for grain packaging.
Automatic Rice Weighing, Packaging & Checkweighing Production Line
Fully Integrated Automated Grain Packaging System
Product Overview
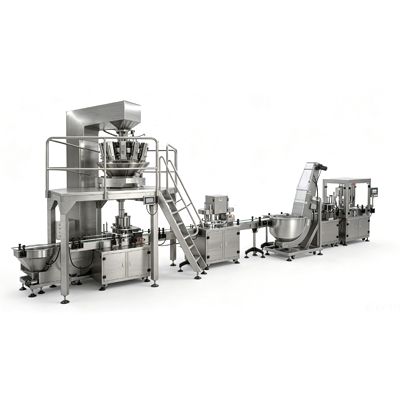
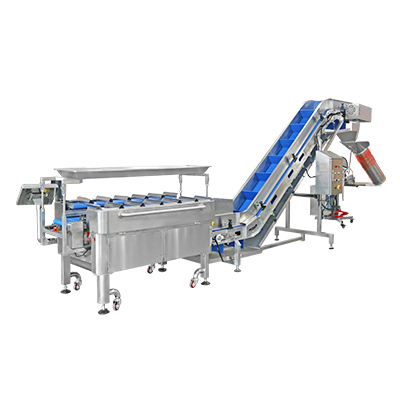
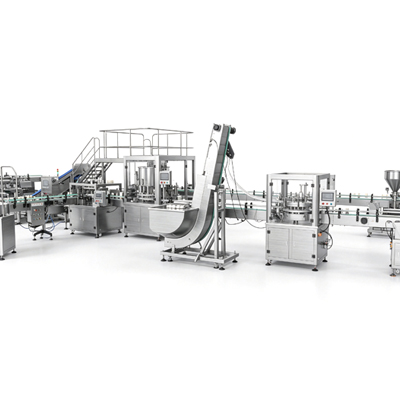
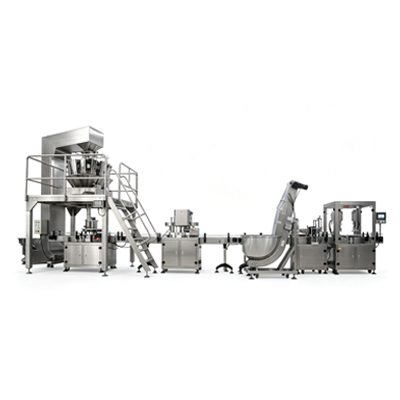
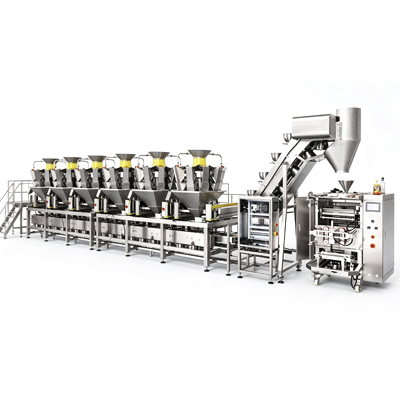
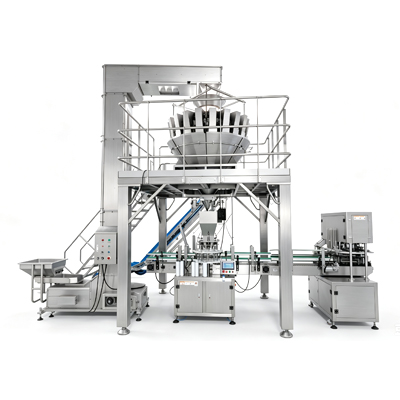
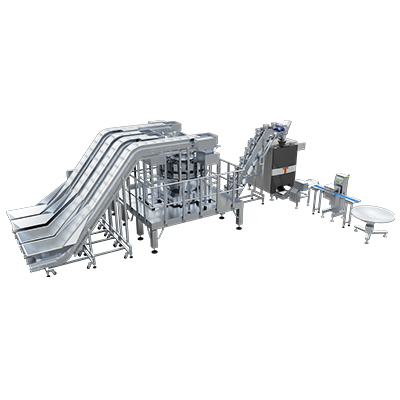
This fully automatic rice weighing, packaging and checkweighing production line is a turnkey integrated solution purpose-built for rice processing operations. It covers the complete production workflow: raw material feeding, high-precision weighing, automatic bagging & sealing, 100% weight verification, and finished product conveying & sorting.
Each station operates in tight synchronization to deliver fully automated, low-labor production. The system minimizes manual intervention, boosts overall throughput, and ensures consistent, reliable packaging quality for rice products.
Standard Equipment Configuration
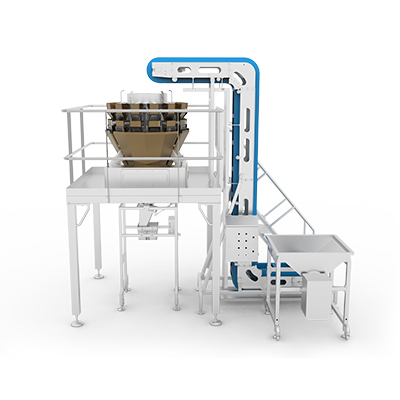
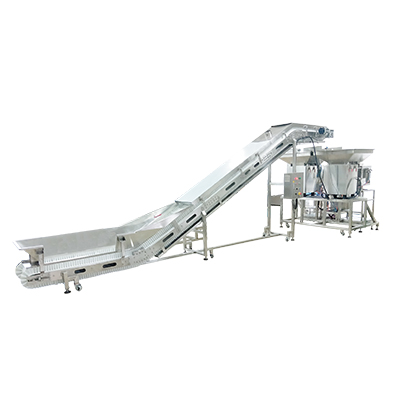
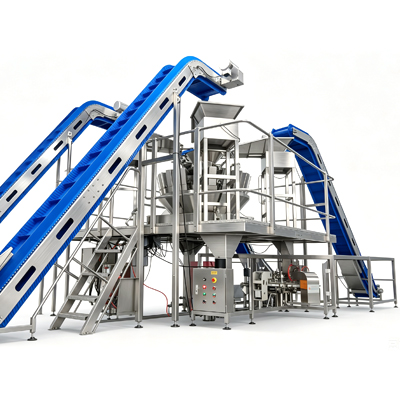
1.8L Z-type Bucket Elevator with Integrated Vibrating Feeder
Delivers stable, uniform raw material feeding and vertical lifting for the weighing system.
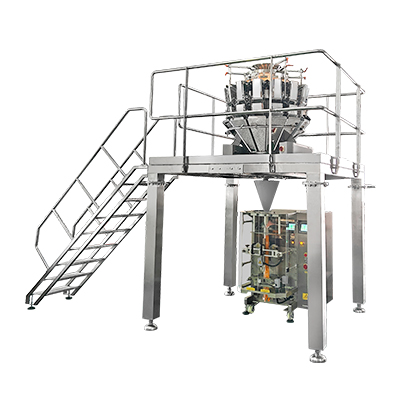
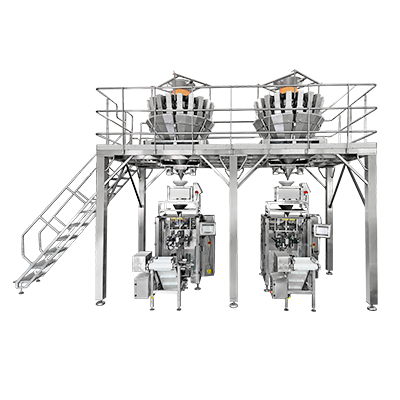
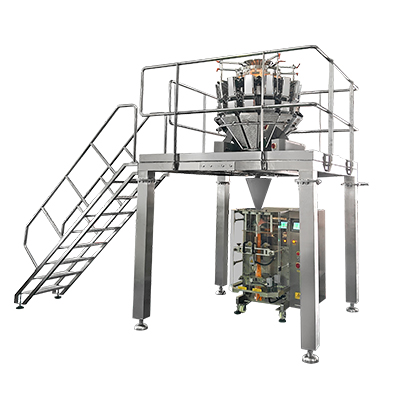
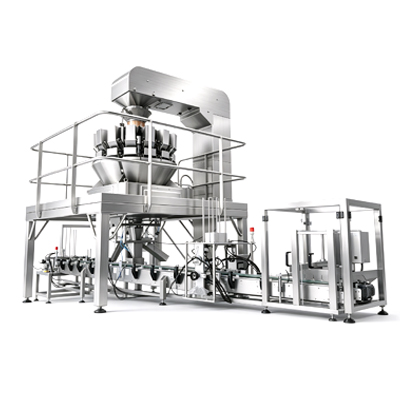
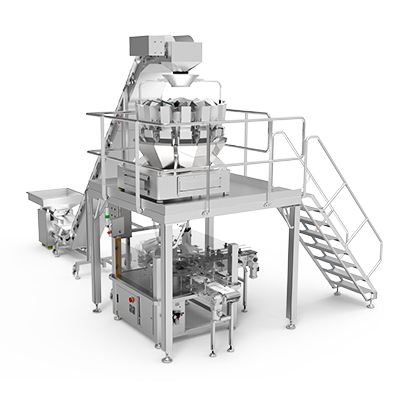
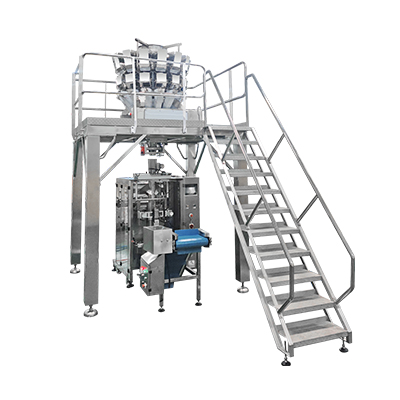
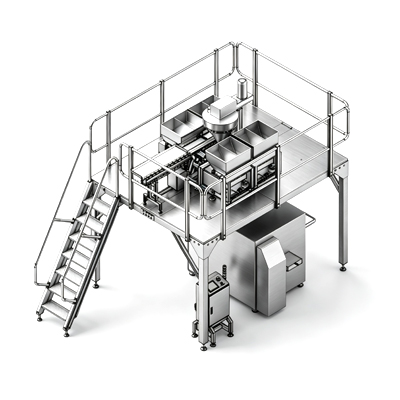
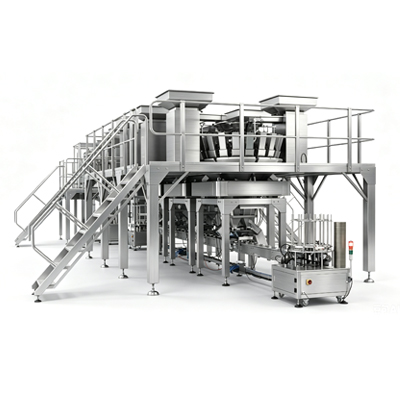
20-head 25-bucket Multihead Weigher
Equipped with 80° inclined chutes, 3° linear vibration pans, and a 200 electric collecting hopper with forced discharge function.
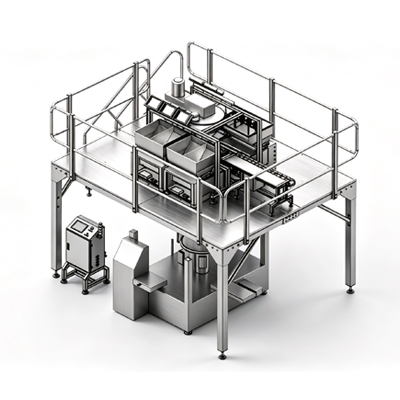
Working Platform
Dimensions: 2500 × 2500 × 2560 mm, providing rigid installation and operation space for the weighing unit.
High-performance vertical packaging unit optimized for granular rice products.
Z-type Finished Product Conveyor
Smoothly transfers sealed packages to the downstream inspection and sorting station.
400 Automatic Checkweigher
High-precision weight inspection system for finished packaged products.
Rotary Sorting & Accumulating Table
For orderly temporary storage and posture alignment of finished packages.
Core System Modules
Precision Weighing Module
The 20-head multihead weigher runs an advanced dynamic intelligent combination algorithm, which rapidly calculates the optimal material combination in each weighing cycle. It achieves a weighing accuracy of +5 g / -2 g, effectively reducing product giveaway and ensuring precise net weight for every package.
Automatic Packaging Module
The vertical packaging machine docks seamlessly with the multihead weigher, enabling fully automated material flow from weighing to bag forming, filling and sealing. Optimized for the physical properties of rice granules, it delivers reliable seal integrity and uniform packaging appearance, with stable continuous output of standard-weight finished bags.
Weight Re-inspection & Quality Control Module
The integrated automatic checkweigher performs 100% full weight inspection on every finished package. Equipped with an intelligent rejection device, it automatically eliminates overweight or underweight unqualified products in real time, ensuring all outgoing units comply with weight specifications.
Conveying & Sorting Module
Z-type Bucket Elevator: Handles vertical lifting and feeding of raw rice, matching the feeding rhythm of the weighing system.
Finished Product Conveyor: Adopts variable frequency speed regulation technology, which intelligently adjusts conveying speed according to downstream operation rhythm to avoid product accumulation or equipment idle running.
Rotary Sorting Table: Provides orderly temporary storage and posture sorting of packaged products, smoothly connects with subsequent secondary packing processes, and improves overall line coordination efficiency.
Key Advantages
Full-Process Automation: Centrally controlled by an industrial control system, the entire line runs automatically from raw material feeding to finished product discharge, significantly reducing manual labor and operating costs.
Remarkable Efficiency Gain: Coordinated operation of all modules increases overall production efficiency by more than 30%, fully meeting large-scale packaging demands of rice processing enterprises.
Dual Quality Assurance: High-precision weighing paired with 100% post-packaging re-inspection creates a dual quality control system, strictly controlling weight accuracy and reducing quality risks.
Material-Specific Optimization: Purpose-designed for rice granular materials, with stable operation, low grain breakage rate, and neat, consistent packaging appearance.
Flexible Production Adaptability: Each unit can be adjusted independently to match different packaging specifications and production rhythms.
Application Scope
This production line is widely suitable for quantitative packaging of various grain granular products including white rice, brown rice, glutinous rice and mixed grains. It is an ideal solution for rice mills, grain processing plants and food production enterprises to upgrade automated packaging and achieve large-scale, standardized production.
Product Description
Submit Your Requirements
Please submit your requirement form, and we will customize the most suitable solution according to your needs.
It is a high-tech enterprise specializing in the R&D, design, and independent manufacturing of packaging, conveying, weight detection, weighing, and filling equipment.